Skip to content

Mobile Pallet Racking System for Cold Storage & Industrial Warehouses

HUADE mobile pallet racking system provides high-density storage for warehouses, cold storage, and industrial facilities. Improve space utilization and efficiency with flexible mobile racking solutions.

Mobile Pallet Racking Overview

What Is a Mobile Pallet Racking System?

Mobile pallet racking is a high-density storage solution designed for heavy-duty pallet storage and efficient use of warehouse space. Pallet racks are installed on electrically operated mobile bases that move laterally along floor tracks.

By using floor-mounted rails and motorized movement, the system requires only a single forklift access aisle instead of multiple fixed aisles. This design reduces wasted space compared with traditional static racks and significantly improves storage capacity.

HUADE provides modular electric solutions that can be customized for different warehouse layouts and storage requirements. The system is suitable for palletized goods in production facilities, distribution centers, and cold storage environments.

Types of Mobile Pallet Racking

Different warehouse requirements require different structural solutions within a mobile pallet racking system:

HUADE Rail-Mounted Mobile Pallet Racking System

Rail-Mounted Type

HUADE rail-mounted mobile pallet racking uses embedded parallel steel rails to ensure smooth movement and high load capacity. It is designed for storing pallets, containers, drums, and other heavy goods, making it an ideal solution for high-density industrial and cold storage warehouses.

HUADE rail-less mobile pallet racking with polyurethane wheels for flexible warehouse storage

Rail-Less Type

Using polyurethane wheels and side guide systems, this design eliminates the need for floor rails and avoids floor reconstruction. It offers flexible warehouse layouts and is suitable for rented warehouses, food processing facilities, pharmaceutical plants, and medical storage environments.

HUADE mobile cantilever racking system for storing film rolls, nonwoven rolls, and plastic roll materials

Mobile Cantilever Racking

HUADE mobile cantilever racking is designed for long and bulky materials such as pipes, steel sections, timber, and panels. The mobile base increases storage density while maintaining direct access, making it ideal for industrial warehouses with oversized products.

Mobile Pallet Racking System Structure & Components

HUADE uses precision-engineered components to ensure smooth movement, high load capacity, and reliable operation. From the rail system and mobile base to the intelligent control panel, each component is designed to improve safety, durability, and long-term warehouse performance.

Guide Rail System

HUADE’s proprietary guide rails are installed along both sides of the racking system to ensure precise positioning and stable movement. The narrow-groove design minimizes vibration when forklifts travel across the rails, improving both safety and operational efficiency.

HUADE guide rail system embedded in the warehouse floor

The flat rail system is developed by HUADE to remain level with the warehouse floor, allowing forklifts and material handling equipment to move smoothly without obstruction while ensuring accurate rack movement.

HUADE Flush Floor Rail

For new warehouse construction, the rail system is installed after the initial concrete foundation is prepared. HUADE engineers precisely level every rail before the final concrete pouring, ensuring smooth rack movement and long-term operational stability.

HUADE integrated rail installation

The mobile chassis is manufactured using HUADE’s proprietary one-piece molding process, providing high structural strength, accurate wheel alignment, and excellent load-bearing capacity without welded joints.

mobile base

Industrial-grade imported motors are mounted below the chassis to prevent contact with pallets during operation while delivering reliable power for smooth rack movement.

Drive motor mounted on the side of the base

The drive shaft synchronizes the motor with the wheels on both sides of the mobile base, ensuring stable and balanced movement throughout the entire mobile pallet racking system.

HUADE rack drive shaft connected to the motor and wheel mechanism

Inside the rack aisle, long limit tabs cooperate with photoelectric switches to set the stop position and distance between racks. This position can be adjusted by relocating the limit tabs.

HUADE stopping limit components with limit plate and sensor inside the rack aisle

Cables are routed inside the rack aisle and clamped by high-elastic foam clamps after positioning. Cables are suspended via special pulley buckles and steel ropes to avoid abrasion during rack travelling.

HUADE suspended cable towing system installed along the rack aisle

The HUADE control panel integrates operation switches, a touchscreen display, emergency stop, and warning indicators into one interface. Operators can open aisles manually or by remote control, allowing forklift drivers to access storage lanes without leaving the vehicle.

HUADE intelligent control panel installed on a movable rack with warning light and electrical control box

Rubber buffer blocks are installed on each rack row to absorb impact and reduce the risk of damage caused by accidental operation.

HUADE shock protection buffer installed at the rack aisle side

Photoelectric sensors monitor aisle entrances and rack movement in real time. If personnel, forklifts, or obstacles are detected, the system immediately slows down or stops to prevent collisions and ensure safe operation.

photoelectric safety sensors for rack movement protection and operator safety

Steel wire mesh decking is installed between all rack beams. Specification: 100Ă—50Ă—5.0mm. Each mesh panel is reinforced with 3 one-piece stiffeners to guarantee safe load capacity.

HUADE steel mesh decking panels installed on rack beams

The steel mesh decking helps prevent pallet misalignment and reduces the risk of small items or molds falling from pallets, improving warehouse safety during storage and handling.

anti-fall safety feature using steel mesh decking to prevent pallet drop

Mobile Pallet Racking System Operating Modes

With flexible configurations and intelligent movement, the system helps warehouses optimize space utilization while adapting to different operational needs.

HUADE full-width aisle mode diagram for a mobile pallet racking system

Full-width aisle mode

Forklifts can quickly access open aisles for fast picking and loading. In combination with guide rail systems and specialized forklifts, aisle space can be further reduced to increase storage density in a high density mobile racking system.

HUADE multi-aisle mode diagram for a mobile pallet racking system

Multi-aisle mode

Allows multiple aisles to be opened at the same time, supporting higher-frequency picking operations in a warehouse mobile racking system.

HUADE even spacing mode diagram for a mobile pallet racking system

Even spacing mode

Designed for inventory management and cold storage applications. Proper spacing between pallet loads improves air circulation and helps enhance refrigeration efficiency in cold storage mobile racking environments.

Key Benefits of Mobile Pallet Racking

Maximize Warehouse Space Utilization

Mobile pallet racking helps increase storage capacity by 60%–100% while achieving over 80% floor space utilization. By reducing unnecessary aisle space, it lowers warehouse construction and energy costs, especially in high-value storage environments.

Safe And Efficient Operation

Equipped with emergency stop buttons, infrared and photoelectric safety sensors, proximity detection, and safety light curtains, the system ensures stable and secure operation. WMS integration is also available to improve pallet storage and retrieval efficiency.

Suitable For Cold Storage And Special Environments

HUADE provides customized solutions for cold storage warehouses, freezer rooms, and explosion-proof environments. The system operates reliably in temperatures as low as -30°C while helping reduce cold air loss and operating costs.

Direct Access To Every Pallet

Unlike compact storage systems with limited selectivity, mobile pallet racking allows direct access to individual pallets without unnecessary product movement, improving operational efficiency and reducing handling time.

Flexible Storage For Different Pallet Types

Supporting pallets of different sizes, weights, and storage requirements, mobile pallet racking adapts to a wide range of industrial applications and warehouse environments.

Intelligent And Energy-Efficient Design

HUADE combines durable racking structures with reliable motor and control technology to create an efficient warehouse mobile racking system that supports long-term, low-maintenance operation.

Multiple Safety Protection Features

Integrated with emergency manual release functions, access control systems, and intelligent safety monitoring, the system improves operational safety and warehouse reliability.

Remote Control Operation

An additional remote control unit enables convenient system operation, providing greater flexibility and improving warehouse management efficiency.

Mobile Pallet Racking System Specifications

Trolley Type Travel Speed Optional Motor Power Optional Control Mode Power Supply Mode Power Supply
2-wheel Trolley, 4-wheel Trolley
Max. 10 m/min
0.4 kW / 0.75 kW
Manual, Automatic, Remote Control
Cable Power Supply
3-phase 5-wire AC380V (50/60Hz) or AC200/220V (Japan)
Safety Devices
Aisle Open Locking
Aisle Entry Protection
Left & Right Buffer Protection
Travel Timeout Alarm
Power ON Interlock between Each Rack Carriage
Motor & Inverter Fault Alarm
Travel Warning Signal
Limit Switch Protection

Is Mobile Pallet Racking Right for Your Warehouse?

A mobile pallet racking system typically requires a higher initial investment than traditional static racking, but it can deliver excellent long-term ROI in warehouses where storage density and space optimization are priorities.

VNA Racking Superflat Floor Icon

Warehouses With Limited Space

For warehouses with limited space or high expansion costs, the system increases storage capacity without expanding the building, maximizing space utilization and efficiency.

Cold Storage & Controlled Environments

Ideal for cold storage and temperature-controlled facilities, it improves storage density while reducing energy consumption and operating costs.

Heavy-Duty Storage Applications

Designed for heavy loads such as steel products, molds, machinery, and automotive parts, it provides stable storage and efficient space utilization for industrial warehouses.

High-Density Warehouse Storage

Ideal for warehouses that prioritize storage density over frequent picking, it supports reserve inventory, bulk storage, and medium-turnover goods in manufacturing and logistics facilities.
Is Mobile Pallet Racking the Right Choice?

Find out whether a mobile pallet racking system matches your warehouse space, storage density, load capacity, and operational requirements.

Get a Free Warehouse Assessment

Whatsapp: +86 18652003451

Our engineers will evaluate your warehouse layout, pallet dimensions, storage capacity, and workflow to recommend the most suitable mobile pallet racking solution—complete with a free layout design and quotation.

Mobile Pallet Racking Project Cases

Explore HUADE mobile pallet racking project cases showcasing customized solutions for different warehouse layouts, storage requirements, and operating environments.

Cold Storage Mobile Pallet Racking Project

Limited Space Challenge

A retail chain needed to increase storage capacity and reduce refrigeration costs in its low-temperature warehouse.

HUADE Solution

HUADE installed a high-density electric mobile pallet racking system with only two operating aisles. The system operates reliably at -25°C and integrates with the existing WMS.

Project Results

The solution increased pallet storage capacity, reduced cold air loss, and improved warehouse space utilization.

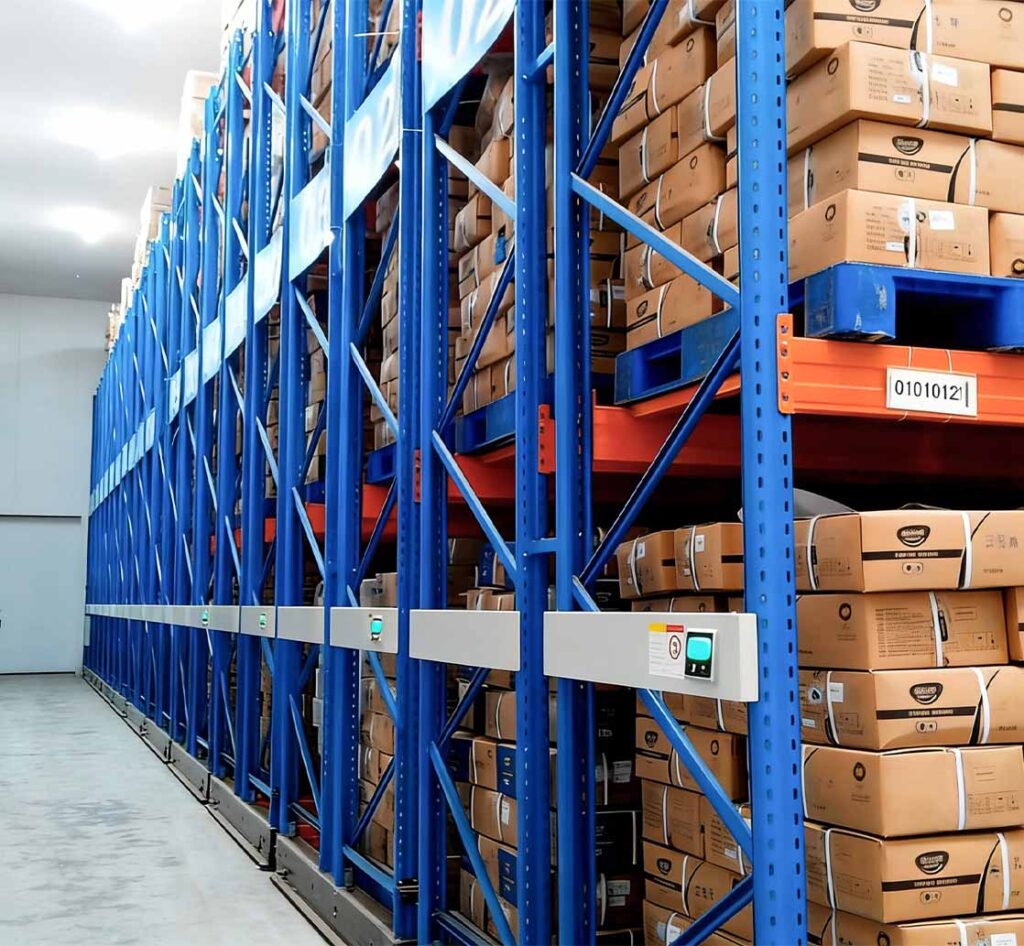
HUADE cold storage mobile pallet racking system for high-density frozen food storage

Project Cases Gallery

HUADE has also delivered mobile pallet racking solutions for cold storage warehouses, manufacturing facilities, logistics centers, and other high-density storage applications across different industries.

Why Choose HUADE for Your Mobile Pallet Racking Solution?

With over 10 years of experience in warehouse automation, HUADE provides customized mobile pallet racking system solutions combining professional engineering, advanced 3D design, strict quality control, and comprehensive project support.

  • Professional Engineering Expertise

    Our experienced designers and project engineers develop high-density mobile racking solutions based on your warehouse layout, storage requirements, and operating conditions.

  • Free 3D Layout & Simulation

    We provide free 3D layouts and simulations to help you visualize the mobile pallet racking system, storage capacity, aisle configuration, and overall warehouse layout before implementation.

  • Strict Quality Control

    Every heavy duty mobile pallet racking project follows strict manufacturing and inspection standards to ensure structural strength, reliable operation, and long-term system performance.

  • End-to-End Project Management

    From engineering design and equipment manufacturing to installation, subcontractor coordination, commissioning, and after-sales service, HUADE provides complete turnkey project support.

  • Training & After-Sales Support

    Our technical team provides system operation training and ongoing after-sales support to help customers operate their warehouse mobile racking system safely and efficiently over the long term.

Get a Customized Mobile Pallet Racking Solution

Looking for a reliable mobile pallet racking system supplier? Contact HUADE Logistics today to design a solution tailored to your warehouse layout, pallet specifications, storage density, and operational requirements.