Chemical Industry Warehouse Solutions
HUADE provides warehouse storage and material handling solutions for chemical manufacturers and chemical warehousing operations. From chemical raw materials and finished products to hazardous materials requiring specialized handling, we help businesses make better use of storage space, improve inventory visibility, and support safer, more efficient warehouse operations.
Key Warehouse Challenges in the Chemical Industry
Chemical warehouses must balance storage capacity, material compatibility, inventory accuracy, and operational safety. Different chemicals may require separate storage areas, specific environmental conditions, and dedicated handling procedures.
As inventory grows, maintaining these requirements while keeping warehouse operations efficient becomes increasingly challenging.
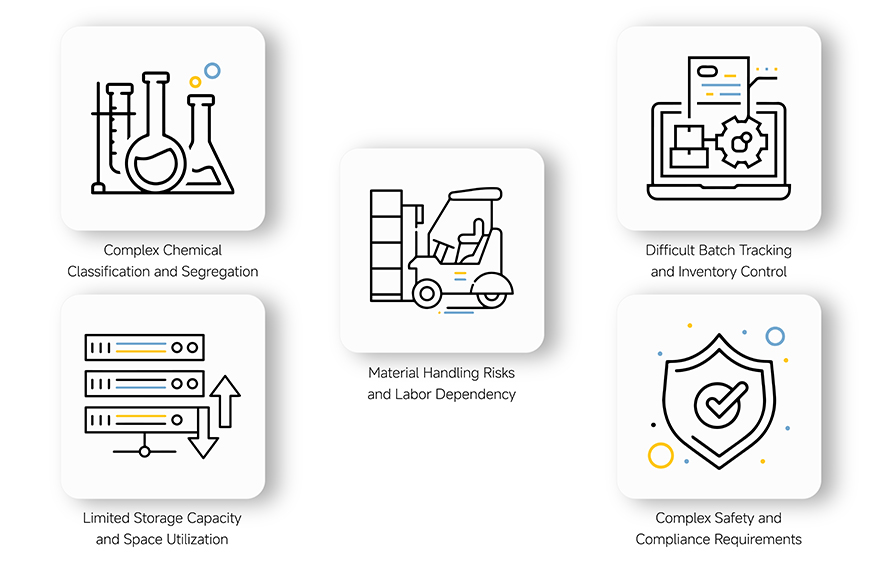
1. Complex Chemical Storage Requirements
Different chemicals may require separate storage areas and cannot always be stored together. Proper classification, segregation, and spill prevention are essential for safer warehouse operations.
2. Limited Storage Space
Forklift aisles and required safety separation take up valuable floor space. As inventory grows, finding room for more pallets without expanding the warehouse becomes a major challenge.
3. Handling and Safety Risks
Working in deep-freeze environments requires appropriate protective equipment and controlled exposure time. Heavy protective clothing can also make manual handling slower and more physically demanding, creating a need to reduce unnecessary human activity inside the freezer.
4. Difficult Inventory and Batch Tracking
Chemical products often need to be tracked by batch number, production date, expiry date, and product type. Manual records make it harder to locate materials, manage stock rotation, and trace specific batches.
5. Complex Safety and Compliance Requirements
Chemical warehouses may need to meet specific requirements for fire protection, ventilation, spill control, and hazardous-area equipment. These requirements vary by material and location, making warehouse planning more complex.
HUADE Chemical Warehouse Solutions
HUADE provides chemical warehouse solutions tailored to storage needs, material characteristics, and handling processes. From flexible racking to automated storage and material handling, we help businesses improve space utilization and inventory management.
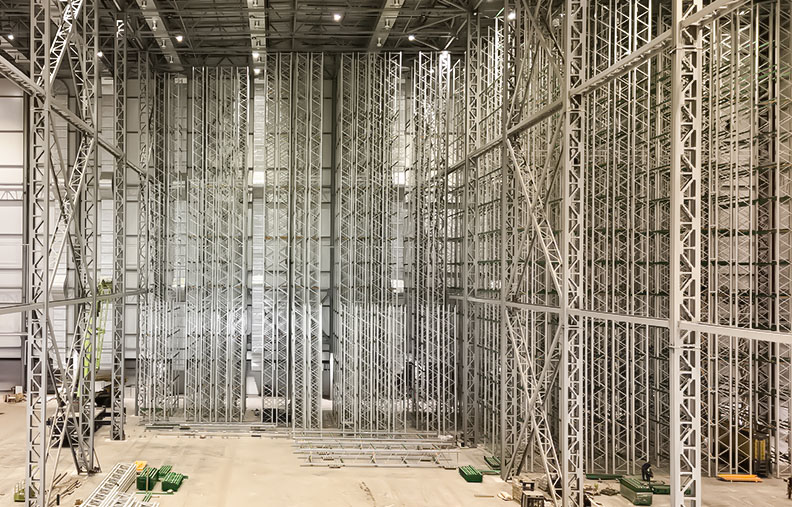
Flexible Racking and Warehouse Layout
HUADE provides Pallet Rack, VNA Racking, and High Bay Warehouse Racking to optimize storage space, organize different materials, and maintain efficient access.
Suitable for: Chemical warehouses with multiple SKUs and different packaging formats.
Automated Storage and Retrieval Systems (AS/RS)
HUADE integrates storage racks, stacker cranes, conveyors, and warehouse software to improve space utilization, reduce manual handling, and support inventory visibility.
Suitable for: Chemical manufacturers handling large pallet volumes or connecting warehouses with production lines.
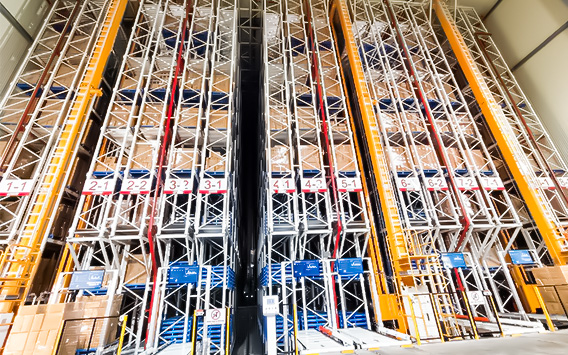
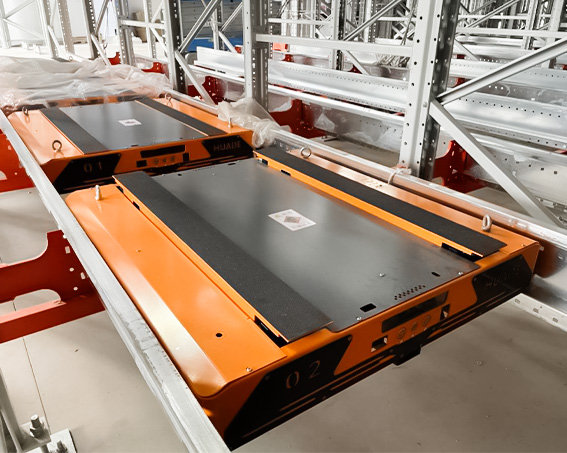
Four-Way Shuttle and Other Pallet Shuttle Systems
HUADE designs pallet shuttle systems to reduce conventional forklift aisle requirements and increase storage density. Each solution is configured for batch management, storage and retrieval frequency, pallet compatibility, and fire protection needs.
For flammable or explosive materials, HUADE evaluates hazardous-area requirements and incorporates suitable explosion-protected equipment and safety measures.
Suitable for: Chemical warehouses requiring high-density storage for batch-based inventory.
Conveyor, Lift, and Warehouse Software Integration
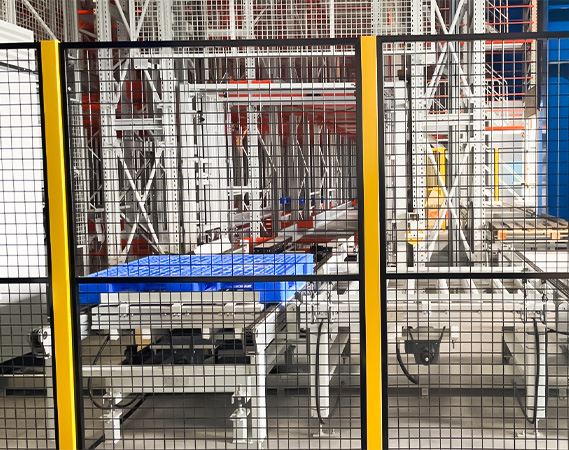
HUADE integrates conveyors, reciprocating lifts, WMS, and WCS to automate material handling.
WCS controls stacker cranes and conveyors, while WMS manages inventory locations and warehouse tasks. This integration reduces manual transfers and improves visibility of inventory and material flows across multiple chemical product types.
Suitable for: Chemical plants with frequent transfers between receiving, production, storage, and dispatch.
Maximize your storage capacity with flexible, high-density Mobile Shelving designed around your needs.
Whatsapp: +86 18652003451
From tailored dimensions and colors to flexible operation and security options, HUADE helps you create the right storage solution for your space.
Chemical Warehouse Project
HUADE designed a high-density four-way shuttle warehouse for a chemical manufacturer. The project includes two storage areas: a conventional warehouse for powder raw materials and finished products, and an explosion-proof warehouse for solvent-based coating materials and finished products.


Project Overview
Conventional Warehouse
- Dimensions: 37 m (L) × 27 m (W)
- Clear height: 26 m
- Storage capacity: 3,204 pallet positions
- Equipment: 4 four-way pallet shuttles and 2 reciprocating lifts
Explosion-Proof Warehouse
- Dimensions: 32 m (L) × 23 m (W)
- Clear height: 28 m
- Storage capacity: 3,052 pallet positions
- Equipment: 4 four-way pallet shuttles and 2 reciprocating lifts
Explosion Protection and Safety Design
Solvent-based materials may create hazardous atmospheres. HUADE therefore incorporated project-specific equipment protection and safety measures for the explosion-protected warehouse.
1. Sealing and Corrosion Protection
Conveyors use 316L stainless steel with mirror-polished inner surfaces. Sealing and protective measures are applied to motors, conveyors, and key lift components to limit exposure to corrosive substances and reduce equipment risks.

2. Spark Prevention
Explosion-protected motors and switches are used on conveyors, lifts, and four-way shuttles to address ignition risks in the designated hazardous areas.
3. Static Electricity Control
Static elimination devices help reduce the buildup of static electricity.
4. Non-Sparking Materials
Selected vehicle and tooling components use non-sparking materials to reduce the risk of sparks caused by mechanical contact.
5. Explosion Protection Certification
The explosion-protected four-way shuttles were specified for the project’s hazardous-area requirements. The applicable certification and equipment protection ratings should be confirmed against the original certificates before publication.
Project Results
The automated shuttle warehouse supports continuous pallet handling, high-density storage, and digital inventory management. Compared with the previous arrangement, the project was reported to deliver:
- Higher storage capacity: Reported increase of 30%–70%
- Space utilization: Reported to reach 95%
- Improved operating efficiency: Reported to double
- Reduced labor requirements: Less manual pallet handling
- Better inventory visibility: WMS and WCS support digital warehouse management and material-flow tracking
Why Choose HUADE for Chemical Warehouse Solutions?
From warehouse planning and equipment design to system integration and after-sales support, HUADE provides tailored chemical warehouse solutions to meet your storage, handling, and safety requirements.
-
Project-Specific Explosion-Proof Design
HUADE has experience in chemical warehouse automation. We configure storage equipment, explosion-proof motors, wireless communication, and power supply systems according to project requirements and applicable explosion-proof standards.
-
In-House Manufacturing and System Integration
HUADE develops and manufactures its own equipment, allowing us to customize designs based on material characteristics and project needs while maintaining control over production quality and delivery schedules.
-
One-Stop Project Delivery
From warehouse planning and software development to equipment manufacturing, system integration, export, installation, and commissioning, HUADE provides support throughout the project lifecycle.
-
Free 3D Layout and Simulation
HUADE provides free 3D layouts and simulations to help customers visualize warehouse designs and review storage configurations before investment.
-
International Project Support
Our engineers can communicate in English and support project documentation and implementation according to destination-market requirements, including applicable regulations and certification needs.
-
After-Sales Service and Technical Support
HUADE provides a one-year warranty, with maintenance plans available after the warranty period. Technical support and software upgrades or modifications are available under the applicable service arrangements.